
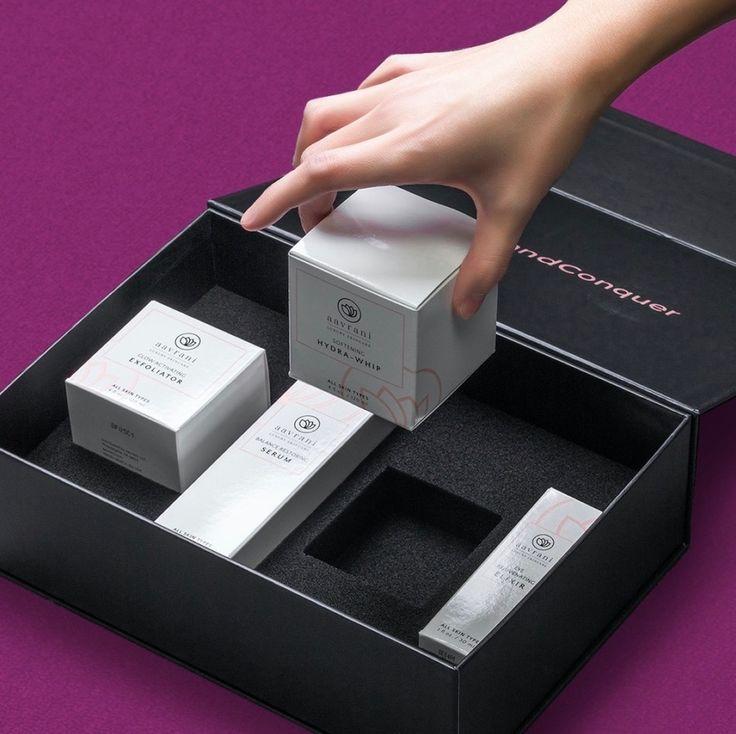
Why Cut Edge Quality Matters in Packaging Inserts
The edges created when packaging inserts are cut may seem like a minor production detail, but they can influence fit, assembly, appearance, and how the insert interacts with the packed product. Different internal packaging formats, including foam, cardboard, corrugated, molded pulp, and other structures, are covered at Inserts Hub, where insert construction is examined as part of the complete packaging system.
Every cavity, slot, opening, finger access point, and outer perimeter contains an edge. The condition of these edges depends on the material, cutting method, tooling, thickness, and design. A clean edge can help components fit as intended, while an uneven or compressed edge may change the finished dimensions.
What Is a Cut Edge?
A cut edge is the exposed surface created when material is separated during production.
In cardboard inserts, this may appear along die-cut openings, tabs, slots, and the outer profile.
Foam inserts contain cut edges around cavities and exterior walls.
Corrugated material exposes paper liners and the internal flute structure when it is cut.
The appearance and behavior of these edges differ because each material has a different internal construction.
Clean Cuts Help Maintain Dimensions
Insert drawings usually contain specific measurements for cavities and structural sections.
The cutting process needs to reproduce those measurements closely.
If material tears outward, compresses inward, or leaves irregular sections around an opening, the usable dimensions can change.
This becomes more noticeable with small products.
A difference that has little effect inside a large shipping insert may create a tight fit around a small bottle, electronic component, cosmetic container, or accessory.
Cut quality therefore contributes to dimensional consistency.
Foam Can React Differently to Cutting
Foam contains a cellular structure that can respond differently depending on the cutting method.
Some cutting processes create relatively smooth cavity walls.
Others may leave more visible texture.
Soft foam can also deform while it is being cut. If the material is compressed during the process, the finished opening may behave differently after the foam returns toward its original shape.
The result can depend on
-
Foam type
-
Density
-
Thickness
-
Cell structure
-
Cavity size
-
Cutting equipment
These factors help explain why two foam inserts using the same drawing may not always look identical if they are produced using different materials or processes.
Narrow Foam Sections Need Careful Cutting
Insert layouts sometimes contain narrow walls between cavities.
These sections can be more difficult to cut because there is less material around them.
A narrow strip may bend during processing or become weaker if the cut passes very close to both sides.
Sharp internal corners can also create concentrated areas where the remaining material is thin.
Designing enough material around openings can help the finished structure remain intact after cutting.
Cardboard Edges Can Show Fiber Layers
When cardboard or paperboard is cut, the internal fiber structure becomes visible along the edge.
This is normal for paper-based material.
However, a damaged or heavily compressed edge can behave differently from a clean cut.
Tabs may become harder to insert into slots.
Small openings may become partially blocked by loose fibers.
Edges around visible openings may also appear less consistent.
The cutting tool needs to pass through the material while maintaining the intended shape.
Corrugated Board Has a Layered Edge
Corrugated material has an additional consideration because it contains flutes between liner sheets.
When the board is cut, the internal flute profile becomes visible.
If excessive pressure crushes the flutes near the edge, the thickness in that area can change.
This may affect parts that rely on the original board depth.
Slots and interlocking sections can be particularly sensitive because their dimensions depend on material thickness.
A slot designed around uncompressed board may fit differently if the edge has been flattened during production.
Cut Edges Can Contact the Product
Not every insert edge remains hidden.
A product may touch the edge of a cavity when it is loaded, removed, or transported.
This can matter when the product has a sensitive finish.
Printed cartons, coated containers, painted objects, polished plastics, labels, and other visible surfaces may respond differently to rough contact.
The relevant question is not simply whether an edge looks clean.
It is also whether the edge is positioned where repeated contact with the product will occur.
Rounded Openings Behave Differently From Sharp Corners
Cavity geometry influences the cut as well.
A rounded corner distributes the change in direction over a wider area.
A sharp internal corner creates a more concentrated transition.
Some materials can reproduce sharp shapes easily, while others may respond better to a small radius.
Foam, paperboard, and corrugated board each behave differently.
The intended product shape should therefore be considered alongside the practical limits of the insert material.
Small Slots Require Dimensional Control
Cardboard inserts often contain narrow slots used for tabs, dividers, or interlocking panels.
These features may only have a small amount of dimensional allowance.
If the slot is too narrow, the adjoining panel may not enter easily.
If it is too wide, the assembled structure may feel loose.
Cutting accuracy becomes especially important where several interlocking sections work together.
A small difference in one slot may influence the position of the connected panel and, in turn, affect another part of the insert.
Tool Condition Can Affect Results
Cutting tools do not remain unchanged forever.
With repeated use, some cutting edges can become less sharp.
A worn tool may produce different results from a newly prepared one.
The exact effect depends on the material and production method.
Possible signs can include more visible fiber disturbance, increased compression, or less defined edges.
Production consistency therefore depends partly on tooling condition as well as the original design.
Edge Quality Matters During Assembly
Insert assembly often involves moving one cut edge past another.
Tabs enter slots.
Divider panels cross through openings.
Walls fold around cut profiles.
If the edges contain excessive material or irregular sections, assembly may require additional force.
This can slow the process or cause the operator to bend a panel differently from the intended direction.
Clean openings help the flat insert transform into its final structure with fewer unexpected contact points.
Cut Quality Can Affect Repeated Use
Some inserts are used once, while others may be opened and handled many times.
Repeated product removal can place additional stress on exposed cavity edges.
A weak foam edge may begin to tear.
A narrow cardboard section can bend.
Loose fibers may become more visible around frequently handled openings.
The effect depends on how the insert is used, but edge condition can influence how well the structure maintains its original form over time.
Samples Reveal Edge Problems
A digital drawing cannot show the physical condition of a finished cut.
This is one reason a production sample can provide useful information.
The sample can be checked for
-
Cavity accuracy
-
Loose fibers
-
Foam tearing
-
Crushed corrugated sections
-
Slot fit
-
Sharp contact points
-
Uneven openings
The actual product can also be loaded and removed several times to see which edges experience contact.
Cut Edges Are Part of the Finished Structure
Packaging insert design often focuses on overall dimensions, material thickness, and cavity layout.
The edges connecting those features are equally physical parts of the insert.
Their condition affects how panels connect, how products enter cavities, and how closely the finished insert matches the drawing.
For that reason, cutting quality should be understood as part of insert construction rather than only as a cosmetic production detail.

 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)